How a laser metal cutting machine fits modern sheet metal production
What a laser metal cutting machine actually does
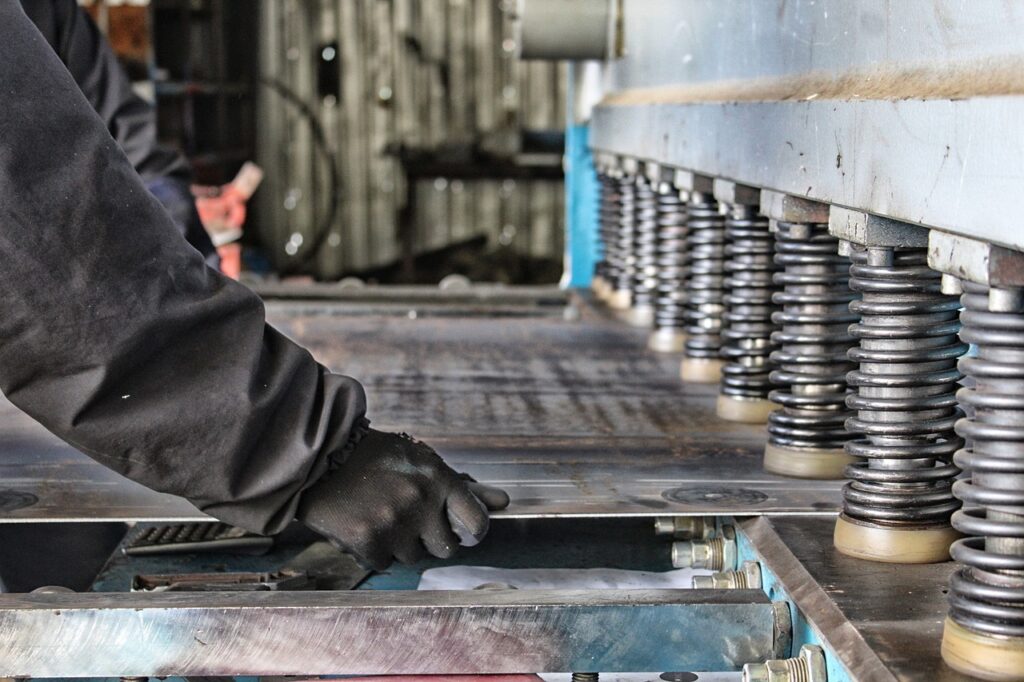
A laser metal cutting machine uses a focused laser beam, CNC motion control, and assist gas to separate metal with a narrow kerf and repeatable geometry. In sheet metal production, its value is not only cutting speed. It is the ability to cut many part shapes without hard tooling, change jobs digitally, and maintain clean profiles when the material, optics, gas, and program are correctly matched.
Fiber laser systems now lead many metal-cutting discussions because they are well suited to steel, stainless steel, aluminum, brass, and copper. Even so, the right choice still depends on thickness range, edge requirements, batch size, automation plans, operating cost, and safety controls.
For manufacturers, the practical question is not whether laser cutting is modern. It is whether the process matches the parts being made. A shop cutting thin stainless brackets all day will judge laser cutting differently from a heavy fabricator processing thick carbon steel plate. This guide focuses on production decisions rather than treating laser power as the only specification that matters.
For more related manufacturing and material-processing topics, see the Materials section.
How the process works
Laser cutting is a thermal separation process. A beam is generated by a laser source, guided to a cutting head, focused into a small spot, and moved along a programmed path. The concentrated energy heats the material locally until it melts, burns, or vaporizes. Assist gas flows through the nozzle to clear molten material from the kerf and, depending on the gas, may also influence the cutting reaction.
The machine is more than the laser source. A production system normally includes the resonator or fiber laser module, CNC motion platform, cutting head, focusing optics, nozzle, gas supply, cooling unit, enclosure, extraction system, nesting software, and safety interlocks. Each element affects cut quality. A high-power source cannot compensate for poor nozzle alignment, contaminated protective glass, unstable gas pressure, or inaccurate focus control.
Three variables are especially important in daily operation:
- Power density: Higher power can increase cutting capacity, but the useful result depends on beam quality, focus position, material absorption, and piercing strategy.
- Assist gas: Oxygen, nitrogen, and compressed air create different edge conditions and cost profiles.
- Motion control: Acceleration, corner handling, path planning, and nesting influence throughput as much as straight-line cutting speed.
This is why experienced fabricators evaluate the complete cutting cell instead of comparing machines only by kilowatts.
Fiber, CO₂, and other cutting methods
Most current metal-cutting investment discussions center on fiber laser systems. Fiber lasers commonly operate near a 1 micrometer wavelength, while CO₂ lasers operate around 10.6 micrometers. Industry guidance from major laser equipment suppliers such as TRUMPF, Bystronic, and IPG Photonics consistently describes fiber lasers as efficient and well suited to metal processing, especially for thin to medium sheet and reflective metals when the machine is properly designed.
CO₂ lasers remain relevant in some manufacturing environments, particularly where a company already owns reliable equipment or processes a mix of non-metal materials. For new sheet metal cutting capacity, however, fiber laser systems are often evaluated first because of their compact beam delivery, reduced optical maintenance compared with mirror-based systems, and strong performance on many metals.
| Process | Where it often fits | Main limitation |
|---|---|---|
| Fiber laser cutting | Thin to medium sheet metal, high mix of part shapes, automated production | Capital cost, gas demand, and sensitivity to setup quality |
| CO₂ laser cutting | Existing production lines, some non-metal or mixed-material applications | More complex beam delivery and weaker fit for many new metal-focused investments |
| Plasma cutting | Thicker plate, structural fabrication, lower equipment-cost applications | Wider kerf and rougher edges compared with precision laser cutting |
| Waterjet cutting | Heat-sensitive materials and parts where no heat-affected zone is desired | Slower throughput and abrasive handling requirements |
| Punching | High-volume sheet work with repeated holes, forms, and standard features | Tooling requirements and less flexibility for complex contours |
The comparison shows why there is no universal best cutting method. A laser metal cutting machine is strongest when flexibility, contour accuracy, narrow kerf, and digital job changeover are worth more than the lowest possible cost per straight cut.
Material and thickness considerations
Material behavior is central to laser cutting. Mild steel, stainless steel, aluminum, brass, and copper do not absorb heat in the same way, and they do not produce the same edge condition with the same assist gas. Even within the same alloy family, surface condition, coating, flatness, mill scale, and internal stress can change the result.
Mild steel
Mild steel is widely processed with oxygen or nitrogen. Oxygen supports an exothermic reaction, which can help cutting speed in carbon steel, but it usually leaves an oxide layer on the edge. That oxide may be acceptable for general fabrication, but it can create additional preparation work before painting, powder coating, or welding. Nitrogen can produce a cleaner, oxide-free edge, but it normally requires higher flow and pressure, increasing gas cost.
Stainless steel
Stainless steel is commonly cut with nitrogen when an oxide-free edge is required. The quality target is often a bright edge with minimal discoloration and burr. The challenge is balancing speed, gas use, focus, and heat input. Excessive heat or an unstable cut can create dross, edge tint, or roughness that affects downstream finishing.
Aluminum, brass, and copper
Reflective metals require careful machine design and process control. Modern fiber systems are widely used for these materials, but reflectivity and thermal conductivity still matter. A stable piercing strategy, appropriate power level, back-reflection protection, and clean optics are important for reliability.
Thickness also changes the decision. Thin sheet may be limited more by acceleration, nesting, loading, and unloading than by raw laser power. Thicker material may require slower speeds, more careful piercing, greater gas consumption, and closer attention to edge taper and dross. Cut charts and sample testing are therefore more useful than a single headline capacity number.
Assist gas, edge quality, and total operating cost
Assist gas is one of the most underestimated cost factors in laser cutting. It affects edge chemistry, dross, surface color, cutting speed, and cost per part. Oxygen, nitrogen, and compressed air each have a place.
- Oxygen: Often used for carbon steel. It can improve cutting action through oxidation, but it leaves an oxidized edge.
- Nitrogen: Often used for stainless steel, aluminum, and applications needing cleaner edges. It can reduce secondary finishing but may raise gas cost.
- Compressed air: Can lower gas expense for some jobs, but the edge may show oxidation or quality variation depending on material and requirements.
Total operating cost includes more than electricity and gas. It also includes protective windows, nozzles, filters, extraction maintenance, cooling, software, operator time, scrap, part sorting, downtime, and service support. A machine that cuts quickly but requires frequent manual intervention may not outperform a slower system with better automation and more stable uptime. See also: Machines.
Edge quality should be judged by the next process, not only by appearance at the cutting table. If a part will be welded, coated, bent, or used as a sealing surface, oxide, burr, taper, and micro-dross may matter. The best cutting condition is the one that supports the full manufacturing route, not just the cutting department’s cycle time.
Automation and software now shape the business case
In many factories, the laser source is only one part of the productivity equation. Loading systems, pallet changers, sheet towers, part sorting, remnant tracking, and nesting software can determine whether the machine becomes a flexible production cell or a bottleneck surrounded by manual handling.
Automation is especially valuable when batch sizes are small and job changes are frequent. A laser can switch programs quickly, but material handling still takes time. If an operator must manually load every sheet, remove skeletons, sort parts, and search for remnants, real throughput may fall below the cutting head’s capability. Good nesting software also reduces scrap, controls heat buildup, supports common-line cutting where appropriate, and organizes part identification.
Current industry discussions also emphasize beam shaping, sensor-based piercing, automatic nozzle changing, focus control, and process monitoring. These features are not just marketing details when they reduce scrap or shorten setup time. They should still be evaluated against the parts a shop actually makes. A simple, reliable configuration may be better for a narrow product range, while a job shop may benefit from broader automation and software integration.
Safety and compliance cannot be treated as accessories
Industrial laser cutting involves optical, mechanical, electrical, fire, fume, and gas hazards. Public guidance from OSHA and NIST points to structured laser safety programs, training, hazard evaluation, engineering controls, administrative controls, and suitable personal protective equipment. ANSI Z136.1 is widely referenced in the United States for safe laser use, while ISO 11553-1:2020 addresses laser safety requirements for laser processing machines and has remained a current reference after review. ISO 11553-2:2026 specifically addresses hand-held or hand-operated laser processing machines, which is relevant as portable laser processing equipment receives more attention.
Enclosed CNC laser cutters are often designed to protect the operator during normal operation. Higher-risk conditions can appear during service, alignment, maintenance, door interlock bypassing, or operation with damaged enclosures. Shops should also assess non-beam hazards. Cutting metals can generate fumes and particulates, and assist gases can introduce pressure and oxygen-enrichment risks if handled poorly. Extraction, filtration, fire prevention, gas storage, and housekeeping are therefore part of the cutting process, not separate afterthoughts.
A practical safety review should include the machine enclosure, interlocks, viewing windows, emergency stops, fume extraction, fire detection, gas lines, pressure regulators, electrical isolation, operator training, maintenance access, and written procedures. The goal is to make safe operation repeatable rather than dependent on individual caution.
How to evaluate a laser metal cutting machine
Before selecting a system, manufacturers should define the production requirement in measurable terms. The following checklist is more useful than starting with laser power alone:
- List the real material mix. Include alloy, thickness range, coating, sheet size, and annual volume.
- Define acceptable edge quality. Consider burr, oxide, taper, surface roughness, and downstream finishing.
- Compare actual part families. Thin nested parts, heavy plates, long straight cuts, and intricate contours stress different machine capabilities.
- Estimate gas and utility demand. Nitrogen supply, compressor capacity, extraction airflow, and cooling can affect installation cost.
- Check automation needs. Loading, unloading, sorting, and remnant handling may determine real output.
- Review software workflow. CAD import, nesting, quoting, scheduling, and traceability can reduce hidden labor.
- Assess service support. Local technician availability, spare parts, remote diagnostics, and operator training affect uptime.
- Plan safety and facility changes. Enclosures, ventilation, fire controls, gas storage, and floor space should be reviewed early.
Sample cutting is strongly recommended when the investment is significant. Test parts should represent real production, including small holes, corners, long contours, tight nests, coated material, and the thickest and thinnest sheets expected. A demonstration using only ideal samples may not reveal the limits that appear in daily work.
Frequently asked questions
Is fiber laser always better than CO₂ for metal cutting?
No. Fiber laser is often the first choice for new sheet metal cutting investments because it performs well on many metals and can offer strong operating efficiency. CO₂ may still be useful in existing installations or certain mixed-material environments. The better choice depends on material, thickness, edge expectations, maintenance capability, and cost structure.
What thickness can a laser metal cutting machine cut?
Capacity depends on laser power, beam quality, machine design, material type, gas, and acceptable edge quality. Published maximum thickness values should be treated as starting points, not guaranteed production conditions. A shop should verify its own materials through sample cuts.
Does higher laser power always reduce cost per part?
Not always. Higher power can increase cutting speed and thickness capacity, but it can also increase capital cost, gas demand, and facility requirements. If loading, unloading, programming, or part sorting is the bottleneck, more power may not improve overall productivity.
Which assist gas gives the best edge?
There is no single best gas. Nitrogen is often chosen for clean, oxide-free edges, oxygen is common for carbon steel cutting, and compressed air can be economical for suitable jobs. The right choice depends on material, coating, finishing requirements, and cost targets.
What is the most common mistake when buying a laser cutter?
The most common mistake is comparing machines by power and purchase price while ignoring gas supply, automation, service, software, extraction, safety, and downstream finishing. The best investment is the system that improves the complete production flow.
Final takeaway
A laser metal cutting machine can be a flexible tool for modern sheet metal production, but its value comes from the full process: laser source, motion system, gas choice, software, automation, safety controls, and operator discipline. Fiber technology has strengthened the case for laser cutting in many metal applications, yet plasma, waterjet, punching, and existing CO₂ systems still have roles where their economics or material fit are stronger. The most reliable decision starts with real parts, real materials, and a clear view of the total manufacturing route.